

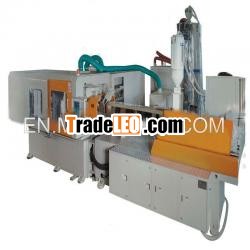
Description:
PP preform injection machine:4 cavity to 96 cavity mould available;
Short cycle time;
Easy Maintenance
PP preforminjection machine
1. High-speed CPU based SiemensSP300 control system withOperator-friendly interfaces assures auto-protection function ofmachine and automatic process control.
2. Profibus-DP communication module allows forinstantaneous response and precise control of themachine hydraulicsystem and robot.
3. Accumulator fromREXROTH provides adequate hydraulicforce.
4. Independent BOSCH servo-valve control of moldclamping, ejection and injection contributes to instantaneous,stable and precise machine movements.
5. Accurate control of mold stroke prolongs moldlife.
6. Specially designed take-off plate shortens robotstroke.
7. SEW servomotors from Germany forthe robot leads to fast and accurate control of robot stroke, whichin turn shortens preform transfer time as well as extending machinelife.
8. Higher machine rigidity with thickerplatens and heavier machine platform enables the machine to runfast but stable.
9. Preform can be accepted in accordance withpeform drawing /confirm/ied.
injection molding machine
Model | TP-32PET | TP-48IVPET | TP-56IVPET | ||
Injection Unit | Screw L/D ratio | L/D | 25 | 25 | 25 |
Screw Diameter | mm | 85 | 100 | 120 | |
Injection Pressure | Kgf/cm² | 1080 | 907 | 907 | |
Machine size (L*W*H) | Mm | 8450×3590×2160 | 9410×4380×2400 | 9410×4380×2400 | |
Shot Volume (Max.) | cm³ | 1700 | 2850 | 2850 | |
Shot Weight | g | 2040 | 3420 | 3420 | |
ors | 72 | 121 | 121 | ||
Clamping Unit | Clamping Force | Ton | 280 | 320 | 320 |
Clamping Stroke | Mm | 545 | 500 | 500 | |
Mold Thickness (min/max) | Mm | 280~700 | 480~780 | 480~780 | |
Tiebar Spacing (W*H) | Mm | 610×610 | 660×860 | 660×860 | |
Ejector Storke | Mm | 150 | 180 | 180 | |
Ejector Force | Ton | 8 | 13 | 13 | |
No.of Ejector Pins | Piece | 5 | 11 | 11 | |
System Pressure (max) | Kg/cm² | 140 | 140 | 140 | |
Preform Mold | Caviation (max.) | Piece | 32 | 48 | 56 |
Preform Length (max.) | Mm | 190 | 190 | 190 | |
Hot-runner | Pneumatic Valve-gate Hot Runner Mold | ||||
Robot | T/O Tubes | Piece | 96 | 144 | 168 |
Installation Power | Pump Motor Power | KW | 45 | 45 75 | 45 75 |
Robot Power | KW | 10 | 25 | 25 | |
Mold Heating | KW | 38 | 42 | 44 | |
Machine Heating | KW | 37 | 71 | 71 | |
Total Power | KW | 130 | 258 | 300 | |
General Requirements | AC Power(3 Phase 4 Line) | V | 380 | 380 | 380 |
| °C | 5~15 | 5~15 | 5~15 | |
Chilling Water | Mpa | 0.8 | 0.8 | 0.8 | |
| L/min | 420 | 600 | 600 | |
| °C | below25 | below25 | below25 | |
Cooling Water | Mpa | 0.25 | 0.3 | 0.3 | |
| L/min | 100 | 200 | 200 | |
Notes: A: Recommended chilling water temperature is 5-15°C B: The data are subject to change for contineousimprovement in technology | |||||
preform molding machine

