

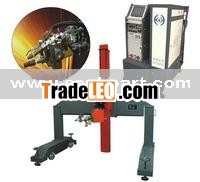
KHBL8-80A Type of 3D adjustment Long Men posture tube–tube sheet automatic pulse argon arc welding
LongMen posture head Host Machine
Applicable industries
Petroleum, chemical, pressure vessel, aerospace, ship, refrigeration, medicine, food machinery, etc
Applicable products
Boiler, pressure vessel, heat exchanger, etc
Applicable scope
Pipe diameter 8mm-80mm carbon steel, alloy steel, stainless steel, copper and copper alloy, and titanium alloy tube-tube plate welding.
Product function and characteristics
1,Suitable for various kinds of tube-tube plate assembly method;
2,3D frame which is fabricated according to adjust with a fifth dimensional tuning, suitable for pipe diameter very center of smaller intensive heat exchanger welding;
3,The welding head can on the surface doing a 180 degree rotated, convenient to replace tungsten pole and wire fine-tuning operation; etc.
4,Head of water, electricity, USES the winding way, welding can continuous rotary, cooperate the arc length adjustment, which can realize multilayer welding;
5, The spindle nose adopts water-cooled positioning, avoid pipe head melts in the flow, welder molding beauty;
6,Driving and wire used stepping motor system, the nose reliable
7,Adopting PLC control system, command nicety, strong anti-jamming capability;
8,Friendly human-machine interface adopts LCD touch screen, all Chinese input simple, intuitive operation, convenient;
9,By Panasonic IGBT inverter control dc pulse power, high efficiency, arc welding strong stability, weld bead molding beauty;
10,Compulsory water-cooling systems, equipped with 16 liters stainless steel water trough, do not suffer site conditions, such as water pressure cooling fully, reliable convenient!
Welding process
Technical parameters
Rated input capacity | 11.5KVA |
Rated input voltage | 380V |
Rated power input | 9.0KW |
Voltage allow fluctuating range | 370V~390V |
Phase number | Three-phase |
Frequency | 50/60HZ |
Rated load sustained rate | 60% |
Rated welding voltage | TIG welding 22.6V |
The rated voltage no-load | 70V |
Weldable tube diameter | 8—80mm |
Weldable wall thickness | 0.5—6.5mm |
Tube biggest stretch out length | 10mm |
Tube biggest indented length | 2mm |
Welding current adjusting range | 4—315A |
The current up time | 0.1—25s |
Current decrease time | 0.1—25s |
Pulse frequency | 0.5—500HZ |
Argon gas flow | 8—12L/min |
Ahead of time instead | 1—25S |
Lag time instead | 1—25S |
Wire adjustable Angle | less or equal to 45 degrees |
Wire feeding speed | 0.1—1.5/min |
Wire filling diameter | 0.8/1.0mm |
Helicopter speed | 0.3—6r/min |
Built-in memory capacity | 100 groups of welding procedure |
Welding speed | 50—150mm/min |
Cooling water pressure | 1.2kg f/mm² |
Tungsten pole adjustable Angle | Less than45 degrees |
Welding effect


